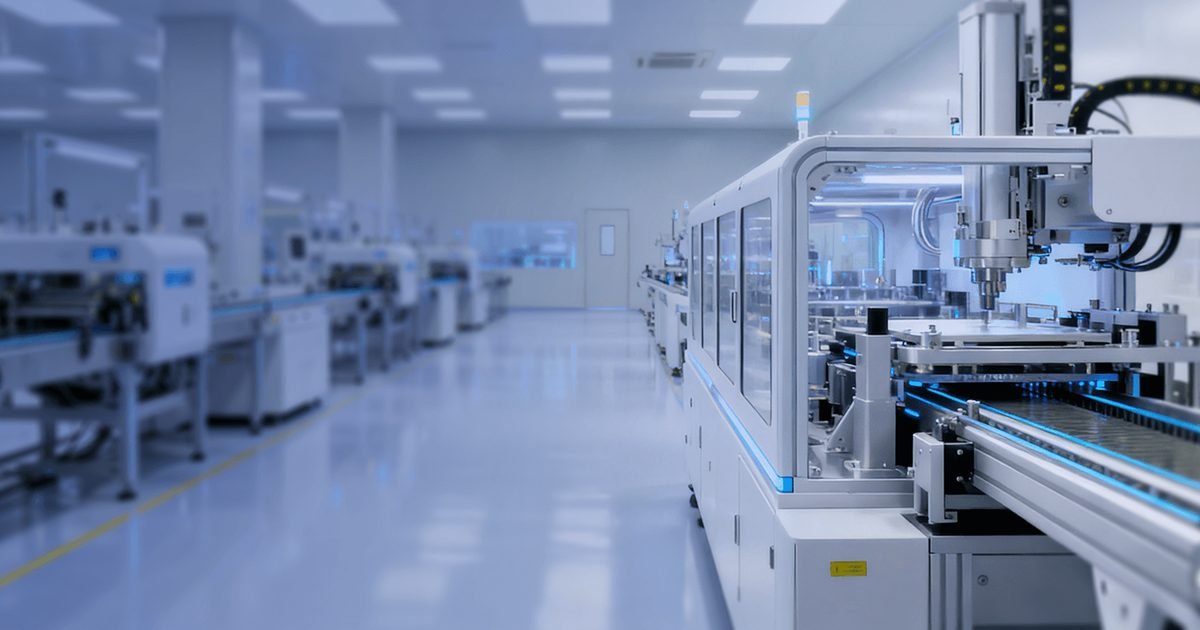
Flux residue that survives the wash line has one cause: the jet never reached it. Residue under a shield can defeats spray and yields to immersion. Five criteria — residue location, geometry, volume, verification, limits — decide whether ultrasonic PCB cleaning or spray cleaning suits your board before you buy.
Our evidence sits on the spray side, because that is what CHUANGQI builds: an inline water cleaning machine (CQ-C9610) that runs wash, DI rinse and hot-air dry in a single pass at conveyor speeds from 0 to 1500 mm/min, and a batch machine (CQ-C743) that sprays at 30–40 psi, dries up to 99 °C and filters both the chemistry and the DI drain at 0.45 µm. Ultrasonic immersion is not in our product line. Where immersion is the right fit for your board, this article says so instead of arguing around it.
Key takeaways
- Spray and immersion fail in different places; choose by residue location, not reputation.
- Spray fits continuous flow: CQ-C9610 runs conveyors from 0 to 1500 mm/min.
- Immersion reaches dense assemblies a jet cannot, but it is a batch tool.
- Five criteria decide it before you spend: residue, geometry, volume, verification, limits.
Two Cleaning Mechanisms, Two Different Failure Modes
This comparison covers flux residue removal on production boards. Machine values quoted below are CHUANGQI’s own product-page specifications, and the immersion side is described by mechanism only, because immersion equipment is not in the CHUANGQI product line.
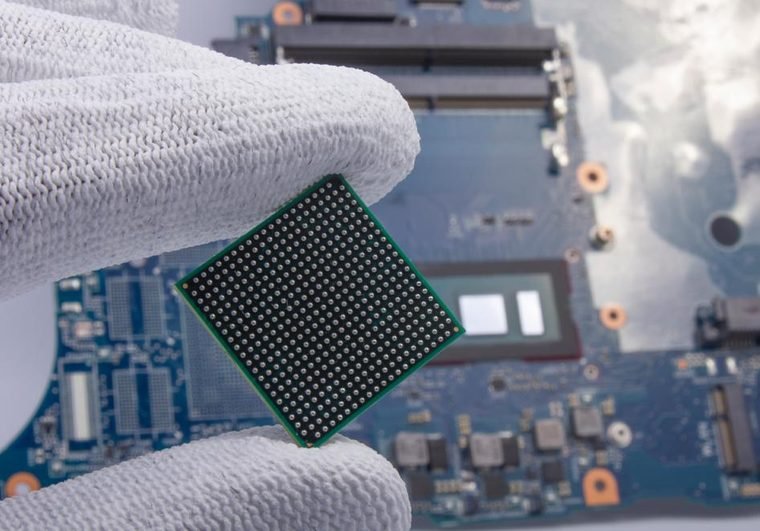
You have probably met the failure already: a ring of residue still sitting under a shield can, same assembly, same machine, third time this month. Spray-in-air and ultrasonic immersion are often compared as if they were two strengths of the same thing. They are not. Each one delivers energy to the board through a different route, so each one has its own way of missing the residue entirely.
Spray-in-air. The machine directs heated wash chemistry at the board, then rinses with DI water and dries with hot air. The mechanism is directional: the jet has to see the surface it is cleaning. That makes the result predictable and repeatable across a production line, and it also defines the failure mode — anything sitting in a jet shadow, behind a tall connector or inside a narrow gap, receives less action than the surfaces around it.
Ultrasonic immersion. The board is racked and lowered into a liquid bath, and cavitation bubbles formed in the bath collapse against the surfaces. The mechanism is non-directional, which is why immersion can clean geometry a jet cannot reach into. The trade-off is that the board has to enter and leave a batch, the liquid does most of the work with less mechanical direction, and some assemblies should not be immersed at all.
Two things follow, and both matter more than the equipment label.
- If your residue sits on open surfaces and your line runs continuously, direction is an advantage, not a limitation.
- If your residue sits under low-standoff parts or inside a dense assembly, the reaching ability decides the outcome, and no amount of jet pressure compensates for a shadow.
Five Criteria That Decide It
Work through the five rows below in order. The first two rows are technical; the last three decide whether the technically correct choice is also the practical one for your plant.
| Selection criterion | Spray-in-air (CHUANGQI line) | Ultrasonic immersion |
|---|---|---|
| Where the residue sits | Strong on surfaces the jet can see; shadowed areas are the known limit | Reaches into dense geometry the jet cannot see into |
| Component geometry | Low-standoff parts and tall connectors create shadows; fixture and nozzle layout compensate | Liquid fills gaps, but part mass and racking decide how much energy arrives |
| Production volume and flow | Inline conveyor 0–1500 mm/min (CQ-C9610); boards move with the SMT line | Batch loads; one cycle is one lot, and it is not suitable for continuous-flow lines |
| Board population limits | Handles a broad component mix, including connectors and heavy copper | Not suitable for assemblies that trap liquid or cannot tolerate batch immersion |
| Verification you can run | Residue checked against the agreed criterion per lot, with a documented acceptance chain | Same criterion, sampled from each batch rather than from a continuous stream |
Source: CHUANGQI specification sheets for the CQ-C9610 inline washer and the CQ-C743 batch washer, with our machine acceptance protocol, 2026-10. Quoted boundaries: conveyor 0–1500 mm/min and detergent draw 1.0–2.5 L/h on the CQ-C9610; 30–40 psi spray pressure, drying to 99 °C and dual-path 0.45 µm filtration on the CQ-C743. The CQ-C9610 runs wash, rinse and dry inside a single conveyor pass; the CQ-C743 runs the same three stages as one closed-loop batch cycle on a two-tier basket. The ultrasonic column describes mechanism only — immersion equipment is not in the CHUANGQI product line.
Three values do most of the work when you write the requirement into an RFQ, whichever method you choose. They also show why the two methods cannot be compared on one number.
| What you specify | Value that matters | Why it decides the call |
|---|---|---|
| Conveyor speed | 0–1500 mm/min (CQ-C9610) | It couples the wash step to your line rate instead of to a demonstration |
| Rinse water | DI water resistivity above 15 MΩ (CQ-C9610 / CQ-C743) | Rinse water sets the residue floor under everything the wash stage achieves |
| Filtration | 0.45 µm on chemistry and DI drain (CQ-C743) | It stops residue that was already lifted from returning to the board |
Source: CHUANGQI product specifications, 2026-10.
Not suitable for every line. An inline spray washer is not the right first purchase for a plant running a handful of dense, high-mix boards a day: you would carry a continuous-flow investment to serve a batch problem, and the fixture work would fall on the same two engineers who already own the line. Equally, immersion is not automatically the answer for a dense board — assemblies that trap liquid, or that cannot go through a batch immersion and drying cycle, remain a verification problem rather than a machine choice. In both cases the honest answer is to clean samples of the real board and look at the residue before committing capital.
Two related pieces are worth reading before you decide. The wash chemistry itself narrows the choice, and water-based versus solvent cleaning covers how to match it to your flux. If the question is really about continuous flow rather than about mechanism, inline versus offline PCBA cleaning machines works through the volume side of the same decision. If you want a machine-level comparison of the spray route, the CQ-C9610 inline PCBA water cleaning machine page lists the full specification referenced above.
Frequently asked questions
Which cleaning method should we choose for PCB cleaning — ultrasonic or spray?
Neither wins in general; they reach different places. Spray gives you direction and repeatability on surfaces the jet can see, which suits open assemblies and continuous lines. Immersion gives you non-directional action that reaches dense geometry, at the cost of batch handling. The deciding factor is where your residue ends up on the board, not which technology sounds stronger.
Which one removes flux residue under BGA and shield cans?
That is the geometry where the two methods separate most clearly. A directed jet loses effectiveness in a shadow, so residue under a package body or beneath a shield can is the classic spray limitation. Immersion reaches those gaps because the liquid fills them, provided the assembly can tolerate a batch immersion and drying cycle. Verify on the real board before you commit to either route.
Can an inline spray washer handle high-mix, low-volume production?
It can run the boards, but high-mix low-volume is where fixtures and changeover dominate the cost rather than cycle time. If your daily volume is small, a batch machine is usually the lower-risk approach, because changeover is a basket and a recipe instead of a line configuration. Volume and mix belong in the decision alongside residue type.
What do we need to send you to get a recommendation?
Send the board or a representative panel, the flux class you solder with, and the residue criterion your customer applies. Tell us the lowest standoff component and the daily volume as well — those two answers move the recommendation more than any other single input. You get a quote within 24 hours together with the technical response, and if a spray route is relevant we clean the board and send back the before-and-after record.
Next step: send your board, the flux class you solder with and your daily volume — we will name the method that reaches your residue, clean a sample to show it, and send a quote within 24 hours — request a cleaning method assessment, or start with a sample cleaning test on your own boards.